
SLA GREY RESIN 3D PRINTING
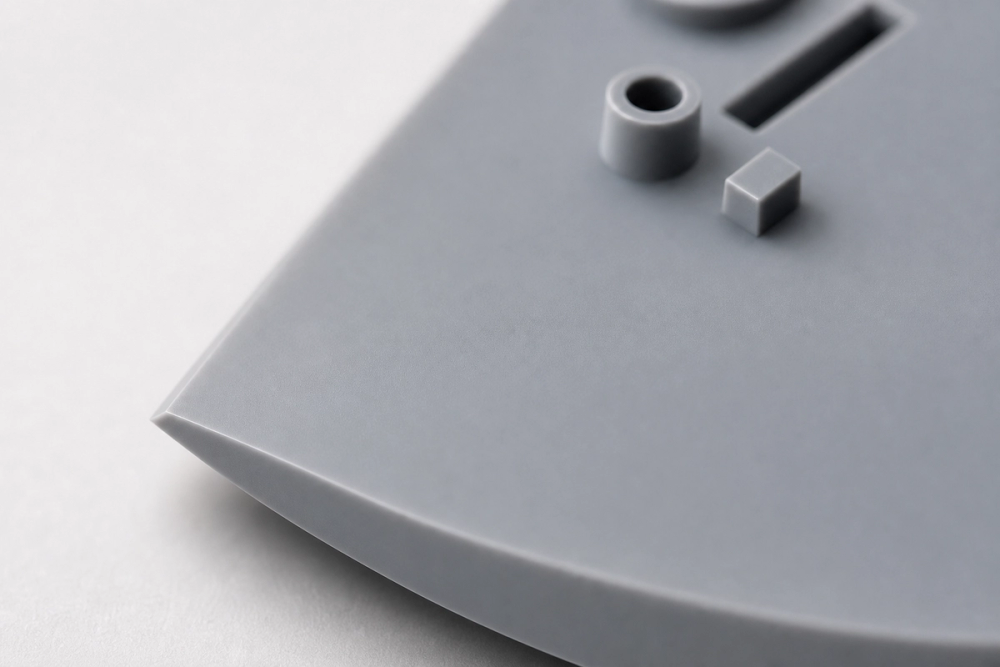
Grey ABS-like resin is Bicester3D's standard SLA workhorse. It cures to a dimensionally stable, paintable, sandable part with the surface finish of an injection-moulded prototype — 0.05mm layer detail straight off the platform, no FDM layer lines. Use it for miniatures, fine-feature prototypes, dental and jewellery patterns, and parts that need to look production-finished without secondary post-processing.
WHEN SLA GREY RESIN IS THE RIGHT MATERIAL
- Surface finish has to look injection-moulded — 0.05mm layers are invisible to the naked eye.
- Tabletop miniatures, jewellery patterns, dental study models — fine detail prints clean off the platform.
- Investor-demo prototypes — visual mock-ups where look-and-feel matters more than function.
WHEN SLA GREY RESIN IS THE WRONG MATERIAL
- Outdoor parts — cured resin yellows and embrittles in UV. Use ASA or PETG.
- Load-bearing structural parts — more brittle than thermoplastics. Use polycarbonate or PETG.
- Large parts — SLA build volume is 200×125×210mm only. Switch to FDM for anything bigger.
SLA OR FDM?
SLA wins on surface finish and fine detail. FDM wins on material range, cost and build size. Most jobs sit clearly on one side or the other.
- ·Surface reads injection-moulded straight off the platform
- ·0.05mm layer detail — invisible at viewing distance
- ·Smaller build volume (200×125×210mm)
- ·Best for miniatures, jewellery, presentation prototypes
- ·Six polymers: PLA, PETG, ABS, ASA, TPU, PC
- ·340×320×340mm build volume
- ·Visible layer lines on the surface
- ·Best for functional, structural, large parts
Pick the right material for your part
SLA grey resin is the default for fine-detail visual work. If your application is functional, outdoor, or rubber-like, FDM materials by use-case are below.
TECHNICAL DATA
| Property | Value | Notes |
|---|---|---|
| Tensile strength | 60–65 MPa | Comparable to engineering thermoplastics |
| Elongation at break | 8–12% | More brittle than FDM |
| Heat deflection temp | 50–65°C | Lower than FDM — not for hot environments |
| Layer height | 0.025–0.1mm | 0.05mm is our default |
| Tolerance | ±0.1mm | Tighter than FDM |
| Surface finish | Smooth, paintable | Layer lines invisible at standard viewing distance |
| Build volume | 200×125×210mm | Formlabs Form 4 — smaller than FDM, split larger parts |
| UV stability | Poor | Yellows and embrittles outdoors |
| Post-processing | Wash, UV cure, sand, paint | Standard SLA workflow |
| Density | 1.18 g/cm³ | Similar to PETG |
WHAT WE PRINT IN SLA GREY RESIN
Representative SLA grey resin work from the workshop queue — every project specified resin over FDM for surface finish, fine detail, or both:
- Tabletop unit sets for an Oxfordshire wargaming designer — 28mm and 32mm scale infantry and vehicle squads, surface detail crisp enough for Citadel-quality painting straight off the platform.
- Investor-demo product mock-ups for a Begbroke spin-out preparing a series-A pitch — enclosure prototypes that needed to look injection-moulded, finished in matte black with metal-effect inserts.
- Architectural presentation models — 1:200 façade detail prints for a Cotswolds heritage planning submission, where window mullions and stone-course detail had to read at viewing distance.
- Jewellery casting masters — lost-wax pattern parts for a small Oxford jeweller, fine geometry surviving the burn-out + casting process intact.
- Cosplay accessory parts — prop weapon detail (handles, hilts, fine etching) where the FDM equivalent would have needed extensive sanding to hide layer lines.
- Dental study models — non-clinical reference models for a regional training programme, gnathic detail clean enough for surface measurement.
PRICING
Per-part SLA pricing from £8. SLA pricing scales with volume and orientation. No minimum order, no setup fees.
Real projects in SLA Grey Resin
Reverse-engineering a ribber dial for a 100-year-old circular sewing machine
GET YOUR SLA GREY RESIN QUOTE
Upload your STL, STEP, or mesh file to the quote tool. Price returns in seconds. Card, invoice (trade accounts) and bank-transfer payment accepted. Most SLA Grey Resin orders are dispatched within 2 working days.
SLA GREY RESIN FAQ
0.05mm layer height is our standard for SLA grey resin — about 1/4 the layer thickness of our finest FDM setting. In practice that means typeface, edges, micro-textures, gnathic detail on dental work, and skin/cloth detail on miniatures all print clean without visible layer lines at normal viewing distance. For finer than 0.05mm we can drop to 0.025mm on request.
Tensile strength is comparable to ABS (60–65 MPa), but SLA resin is more brittle than thermoplastics — 8–12% elongation at break vs 100%+ for PETG. For load-bearing structural parts under impact, FDM (PETG, polycarbonate) is the right call. For visual prototypes, fine-detail parts and casting masters where strength is secondary, grey resin is the standard.
Yes. Grey resin sands and paints cleanly — it's actually one of the easier materials to finish. Standard process: wash in IPA, UV cure, sand at 400–800 grit if needed, prime with rattle-can plastic primer, then paint with acrylic, enamel or rattle-can. Common workflow for cosplay, tabletop minis and presentation prototypes.
Our SLA build volume is 200×125×210mm — significantly smaller than our FDM 340×320×340mm. For larger parts we either split the model into bondable sections (we can advise on cut lines) or print in FDM if surface finish allows. Most miniatures, jewellery, dental and small-prototype work fits inside the SLA volume comfortably.
No to both. Cured photopolymer resin yellows and embrittles under UV — visible degradation within weeks of outdoor exposure. For outdoor use, ASA or PETG are the right choices. For food contact, the photoinitiators in cured resin make it unsuitable, and Bicester3D doesn't certify any printed parts as food-contact safe regardless of process.